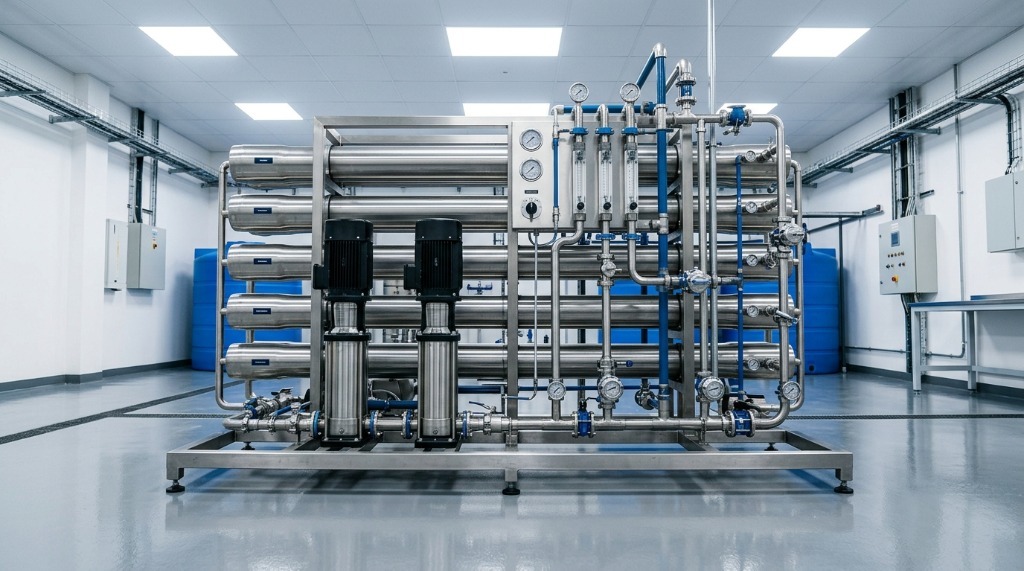
Industrial RO Water Treatment Plant
High-Volume Reverse Osmosis for Manufacturing & Process Utilities
Tailored for challenging feed-water chemistries and intensive industrial operating schedules, our industrial RO treatment plants deliver continuous demineralized and low-conductivity water. Designed after thorough water-quality testing, incorporating chemical dosing, anti-scalant systems, micro-filtration, and automated CIP (Clean-In-Place) flushing modules.
Technical Specifications
* Note: Operating parameters, membrane sizing, and dosing systems can be customized to match your local laboratory water analysis.
Recommended Applications
- Manufacturing & Processing Plants
- Boiler Feed & Cooling Tower Make-Up Water
- Pharmaceutical & Chemical Formulations
- Food & Beverage Processing Facilities
Engineered Advantages
- Heavy-duty multi-stage reverse osmosis design
- Chemical anti-scalant dosing system to preserve membrane longevity
- Integrated Clean-In-Place (CIP) flushing and sanitization manifold
- PLC-based electrical control panel with digital touchscreen HMI
- Comprehensive instrumentation for flow, conductivity, pH, and pressure
Explore Related Water Solutions
Engineered systems tailored for similar water treatment demands.
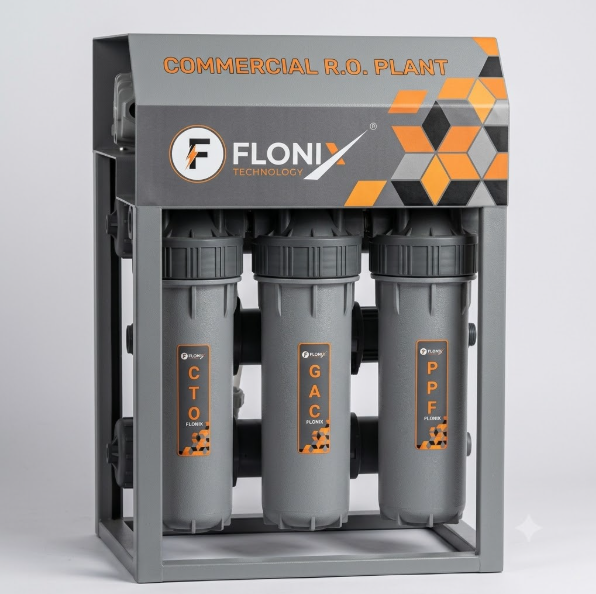
25 LTR Commercial R.O. Plant
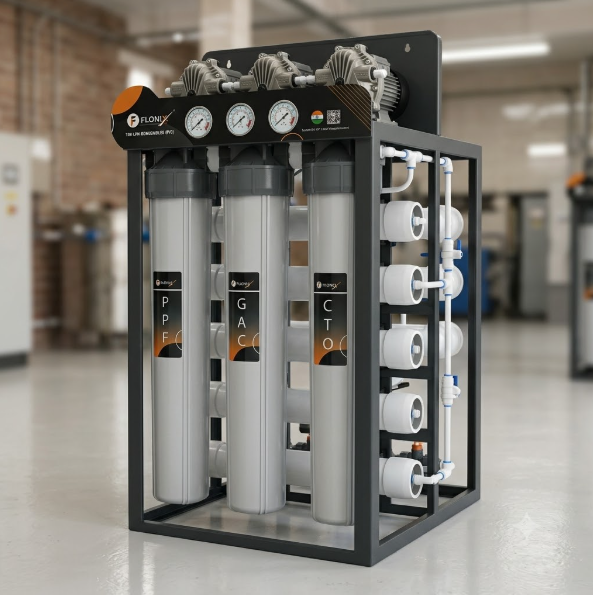
100 LTR Commercial R.O. Plant
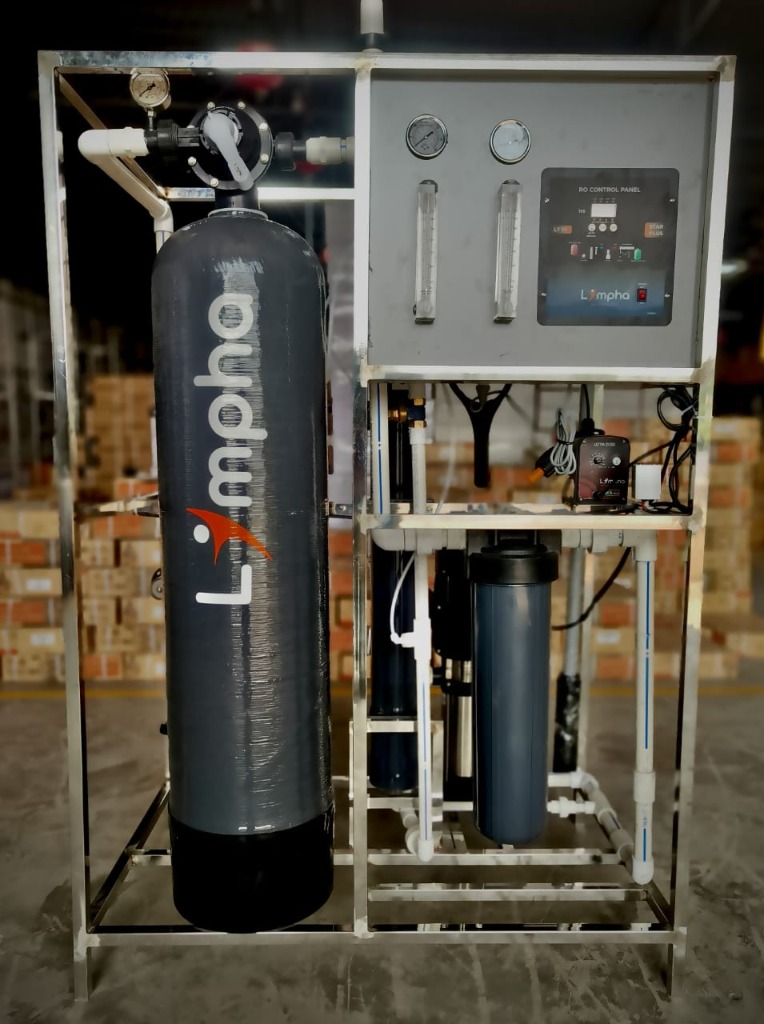
Limpha Commercial RO Plant
Need Expert Sizing or On-Site Water Testing?
Our engineers inspect your raw water TDS, iron, and hardness levels to customize the exact reverse osmosis, softener, or filtration unit for guaranteed results.