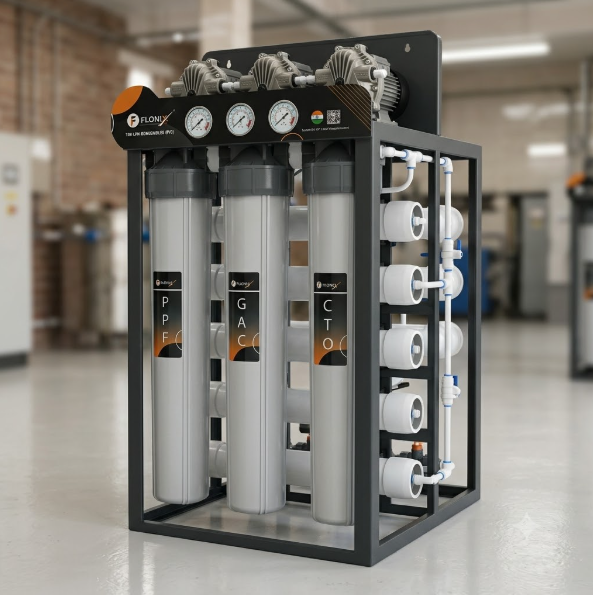
100 LTR Commercial R.O. Plant
Continuous Heavy-Duty 100 LPH Commercial Reverse Osmosis System
The Flonix 100 LTR Commercial R.O. Plant is built for demanding commercial and institutional facilities requiring 100 liters per hour of continuous, high-purity drinking water. Featuring a heavy-duty floor-mounted tubular steel skid, triple high-pressure booster pumps, analog pressure monitoring gauges, and an industrial multi-stage filtration train (20-inch PPF Sediment, Granular Activated Carbon, and CTO Carbon Block preceding high-rejection RO membrane vessels). It effortlessly removes turbidity, chlorine, dissolved solids, heavy metals, and bacterial contaminants with exceptional uptime and service life.
Technical Specifications
* Note: Operating parameters, membrane sizing, and dosing systems can be customized to match your local laboratory water analysis.
Recommended Applications
- Hotels, Restaurants & Commercial Kitchens
- Schools, Colleges & Training Institutes
- Hospitals, Clinics & Diagnostic Centers
- Offices, Factories & Manufacturing Units
- Large Commercial Establishments
Engineered Advantages
- 100 Liters Per Hour high-output continuous purification
- Continuous heavy-duty performance engineered for round-the-clock reliability
- Industrial-grade multi-stage filtration (PPF + GAC + CTO + High-Rejection RO)
- Triple commercial-grade booster pumps with independent pressure gauges
- Heavy-duty powder-coated steel tubular skid frame
- Dual RO membrane banks with quick-service manifolds
- Handles high TDS borewell and municipal water up to 2,000 ppm
Explore Related Water Solutions
Engineered systems tailored for similar water treatment demands.
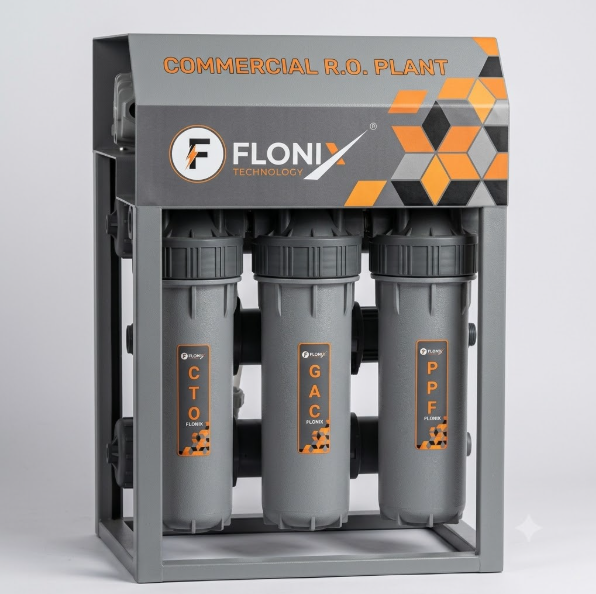
25 LTR Commercial R.O. Plant
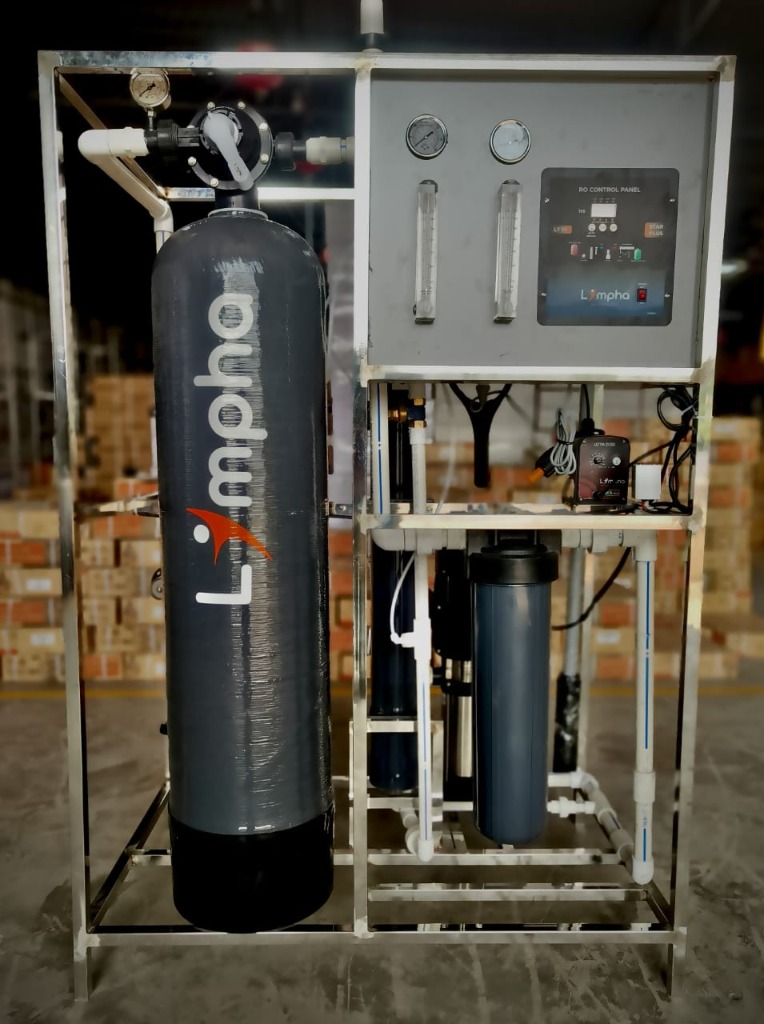
Limpha Commercial RO Plant
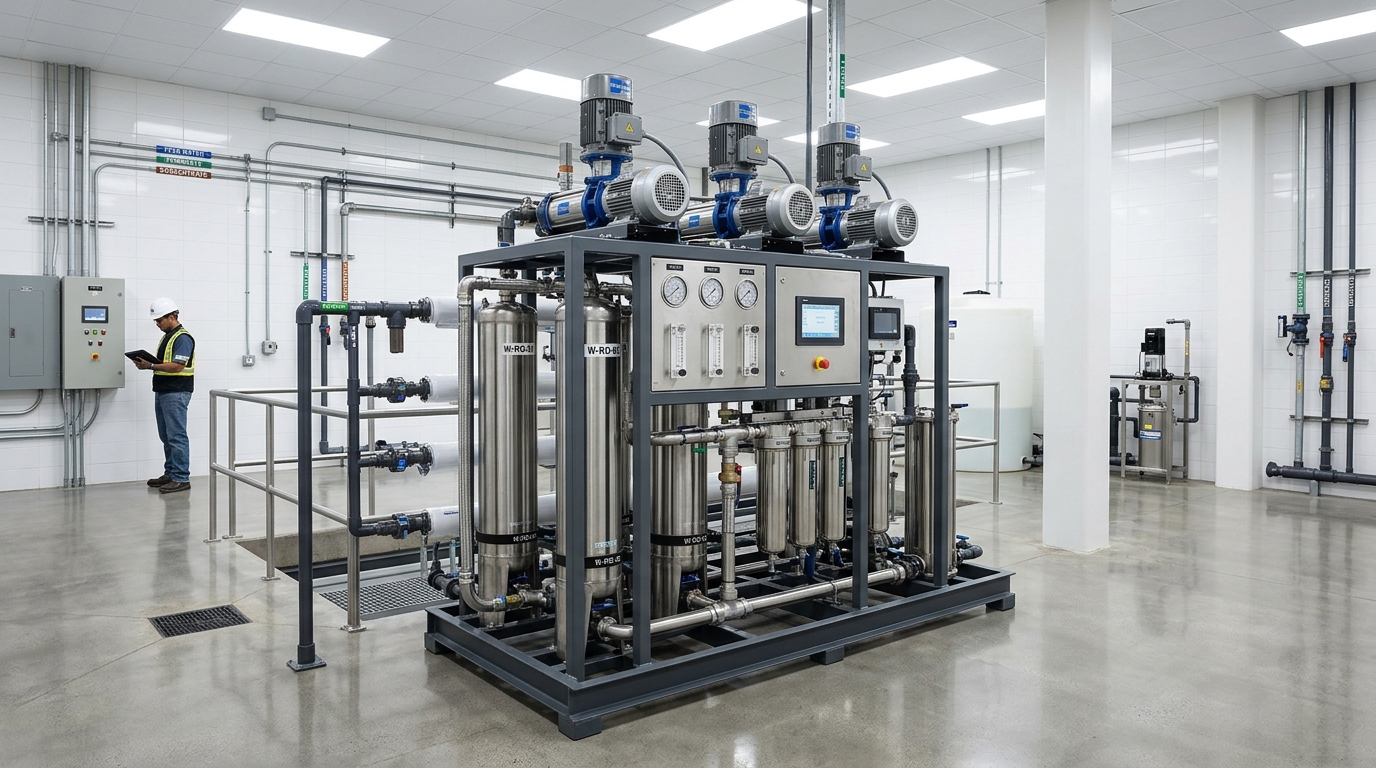
Commercial RO Water Purification System
Need Expert Sizing or On-Site Water Testing?
Our engineers inspect your raw water TDS, iron, and hardness levels to customize the exact reverse osmosis, softener, or filtration unit for guaranteed results.